Building Digital Traceability Into Automotive Component Manufacturing
Automotive suppliers are under constant pressure to deliver consistent parts, respond quickly to quality concerns, and prove what happened during production. A traceability system is the practical link between those demands. It records the journey of a component—from incoming material and machine settings to inspection results, packaging, and shipment—so that a manufacturer can investigate a problem without relying on incomplete paperwork or memory.
What traceability means on the production floor
Traceability is often described as the ability to follow a product forwards and backwards through the supply chain. In a manufacturing setting, that definition becomes more specific. A plant should be able to identify which material batch was used for a particular serialised component, which work order produced it, which equipment processed it, and which measurements confirmed its conformity.
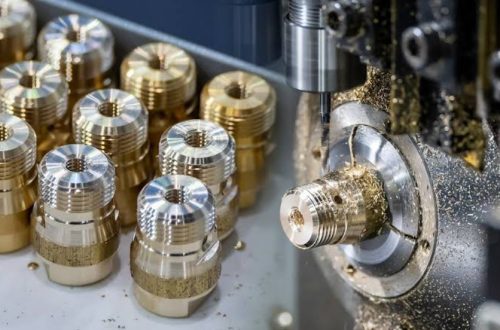
For a machined brake component, for example, the record may include the steel heat number, CNC program revision, tool-life status, operator identification, dimensional inspection readings, wash-cycle confirmation, and packing date. For a battery module, it may extend to cell serial numbers, torque data, electrical test results, and environmental conditions. The required depth depends on the risk associated with the part and the expectations of the customer.
Why automotive manufacturers need detailed records
A defect discovered after shipment can become expensive very quickly. Without reliable records, a supplier may have to quarantine a broad range of stock or issue a recall affecting far more vehicles than necessary. With accurate traceability, the team can narrow the investigation to a defined production window, material lot, machine, or process change.
This containment capability is valuable, but it is not the only benefit. Traceability also supports everyday operational decisions:
- Faster root-cause analysis: Engineers can compare failed parts with process data instead of beginning with assumptions.
- Controlled change management: Revision histories show when a program, fixture, specification, or inspection method changed.
- Supplier accountability: Incoming material and purchased-component records make it easier to isolate external issues.
- Audit readiness: Documented evidence supports customer audits and quality-management requirements.
- Lower waste: Identifying the true scope of non-conforming production prevents unnecessarily scrapping good inventory.
The important point is that traceability should not be treated solely as a compliance exercise. Used properly, it becomes an engineering data source that reveals variation, recurring bottlenecks, and weak points in process control.
Choosing the right identification level
Not every product needs individual serial-number tracking. A high-volume fastener may be tracked by material lot, shift, production line, and container number. A safety-critical steering or braking part may require a unique code on every component. The correct approach balances risk, customer requirements, production volume, and the cost of data capture.
There are three common levels. Lot traceability associates a group of products with a common material or process batch. Batch traceability is useful where products are made in a defined run, such as a moulding cycle or heat-treatment load. Unit-level traceability creates a digital history for every individual part. Many automotive plants use a combination: raw material is tracked by heat or lot, while finished critical assemblies receive unique serial numbers.
Capturing useful data without burdening operators
Traceability fails when it becomes a manual paperwork exercise that operators must complete under time pressure. Handwritten records can be difficult to read, easy to omit, and hard to search during an urgent investigation. The better approach is to capture information as close as possible to the event that creates it.
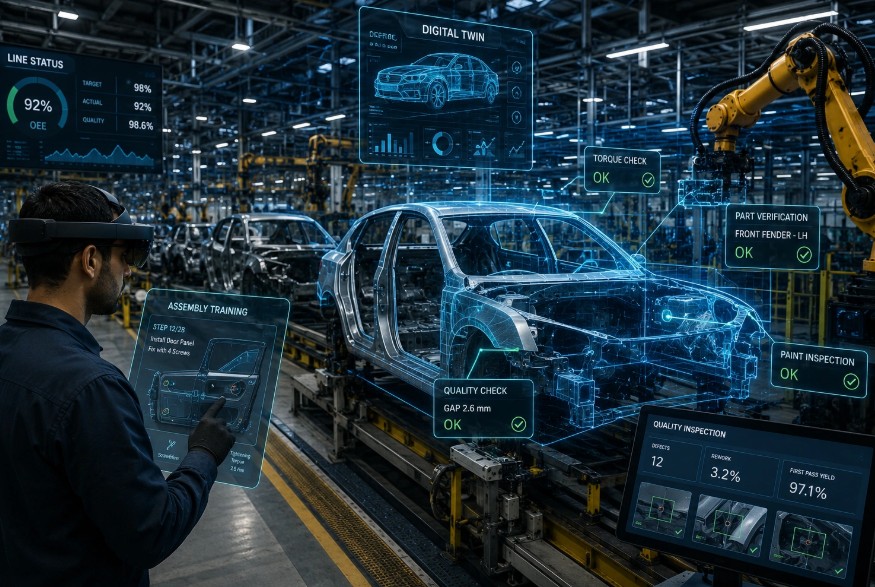
Barcode and RFID scanning can connect a material container to a work order in seconds. Machine interfaces can automatically collect cycle times, parameter values, alarms, and program versions. Inspection stations can send measurements directly from gauges or vision systems. Where manual entry remains necessary, screens should use simple prompts, validation rules, and clear reason codes rather than free-text fields.
A manufacturing execution system can bring these records together, linking production activities with inventory and quality data. However, software alone does not solve the problem. The data model must reflect the real route a part takes through the factory, including rework loops, split batches, component substitution, and outsourced operations.
Implementation steps that reduce risk
- Map the product journey. Document each point where material is received, transformed, inspected, moved, or combined with another component.
- Define the investigation questions. Ask what information the team would need if a customer reported a defect six months after delivery.
- Set a practical data standard. Specify identifiers, ownership, retention periods, and the acceptable method of capture for each process step.
- Pilot on one product family. A limited trial exposes scanning issues, label durability problems, and gaps in workflow before a plant-wide rollout.
- Train for exceptions. Employees need clear procedures for damaged labels, rejected parts, rework, system downtime, and mixed containers.
- Test retrieval regularly. Select a shipped unit and verify that its full production history can be found quickly and accurately.
Data quality is more important than data volume
It is tempting to collect every available signal from connected equipment. Yet a large data set with unreliable timestamps, inconsistent identifiers, or unclear ownership can slow an investigation rather than improve it. Manufacturers should focus first on data that supports product genealogy and process decisions: material identity, process route, critical parameters, inspection status, and release approval.
Common standards matter as well. If one department calls a production order a “job” and another uses a different number for the same work, the digital chain breaks. Master-data discipline, stable part numbering, and controlled revisions are therefore just as important as scanners and dashboards.
Sharing traceability lessons across the sector
Plants often learn the most from practical accounts of failed pilots, label-selection problems, integration choices, and successful containment exercises. Engineers preparing a detailed industry perspective for external readers can explore avenues to purchase guest posts when they need a suitable publishing route. The useful contribution is not a sales message; it is a clear explanation of the methods, constraints, and measurable outcomes that other manufacturing teams can apply.
Conclusion
Effective traceability gives automotive manufacturers confidence in the history of every product they ship. It limits the reach of quality incidents, shortens investigations, and creates a stronger foundation for continuous improvement. The most successful systems are not defined by the number of codes scanned or databases installed. They are defined by whether a team can answer a customer’s question quickly, accurately, and with evidence from the production process.